
Time to read: 12 min
Machine downtime comes at an exceptional cost for manufacturers. Siemens’ True Cost of Downtime study reported the cost of a lost production hour at $36,000 in fast-moving consumer goods (FMCG) and up to $2.3 million in automotive manufacturing. Whether a stop is planned or not, a slow repair makes it longer, and every added hour of idle line is a cost.
The extent to which your own field service team is plagued by downtime depends on how quickly they can perform the necessary service, and that starts upstream. It all begins with the design decisions made in the first weeks of a machine program, before tooling is cut, before the Bill of Materials (BOM) is frozen, and long before the first service call. The way each part is designed has serious implications for the downtime it carries—a hidden expense you won’t find listed in the total cost ledger.
Design for serviceability (DFS) reduces downtime and mean time to repair (MTTR) by making components easier to access, replace, align, and reassemble through deliberate mechanical design decisions made early in development. Design for serviceability and design for maintainability are often used interchangeably in practice across the industry.
This article examines how to make these decisions early in the design process, accounting for the cost of service events over the machine’s service life.
The High Cost of Machine Downtime
Machine downtime costs manufacturers money through lost production, repair labor, and restart delays. The exposure tends to increase with line integration because a single stopped machine can halt everything downstream.
At the top of Siemens’ range, an hour of automotive downtime costs roughly $600 a second. Siemens estimates an idle line at a large automotive plant costs $695 million a year, 1.5 times higher than five years earlier. In heavy industry, the 2024 report puts the cost of an idle plant at $59 million a year, 1.6 times higher than in 2019.
At this scale, the direct price of a $450 cam follower is immaterial. A six-minute delay extracting a seized dowel pin that has no designed-in removal feature burns through more than $230,000 at the automotive rate.
The design implication doesn’t depend on the highest figure to make its case. Let’s say an unplanned service event costs $10,000 per hour in lost production. If a design choice adds two hours to the average replacement time across the installed base, that choice carries a $20,000-per-event price tag that never appears on the part drawing. Over a five-year service life with even a modest failure frequency, the compounding cost of slow replacement can easily outweigh any unit-price savings from simpler part geometry.
Serviceability is an engineering economics problem before it is an ergonomics one.
The pressure to reduce downtime shows up in our own data. 97% of leaders surveyed in our most recent State of Manufacturing Report are prioritizing uptime and maintenance improvements over the next 12 months. At the same time, 89% are facing obstacles keeping equipment running. These include aging machinery/components, finding skilled technicians, and sourcing replacement parts fast enough.
Each Part Plays a Role in Minimizing Downtime
The purchase price of a single component, like a machined bracket, bearing housing, or wear plate, isn’t always the most consequential line item on its total cost ledger.
For an industrial equipment builder or OEM, each component carries a lifecycle liability. This includes field service hours, warranty accruals, expedited air freight for low-volume spares, and, most critically, lost production for the customer.
A split-collar housing designed for a 15-minute bench swap delivers a vastly lower Total Cost of Ownership (TCO) than a one-piece housing that requires a production pause and four-hour driveshaft teardown, even if the split-collar geometry costs 40% more to machine upfront.
When manufacturers select parts on purchase price alone, without considering their serviceability and maintenance implications, they set themselves up for higher downtime costs down the line.
Top Design For Serviceability Principles
Designing for serviceability is a systematic, economics-driven discipline that balances production methods, assembly geometry, and the realities of field maintenance.
Fastener Envelope and Driver Consolidation
A machine that reaches the field with ten different fastener types and three specialized tools cannot be serviced quickly under pressure. Fastener standardization where possible is the highest-leverage starting point.
- Prioritize Fastener-Type Reduction: A company whose technician is hunting for the right driver while a $10,000-per-hour line sits idle is paying for a design decision made months earlier. Minimize the number of fastener sizes per machine.
- Prohibit Mixed Drives: Standardize exclusively on high-torque metric socket head cap screws.
- Mandate Hardware Retention: For nonstructural components, specify captive screws or 1/4-turn quick-release fasteners. Dropping loose fasteners can convert simple preventative tasks into major overhauls.
Poka-Yoke Alignment and Blind Handling
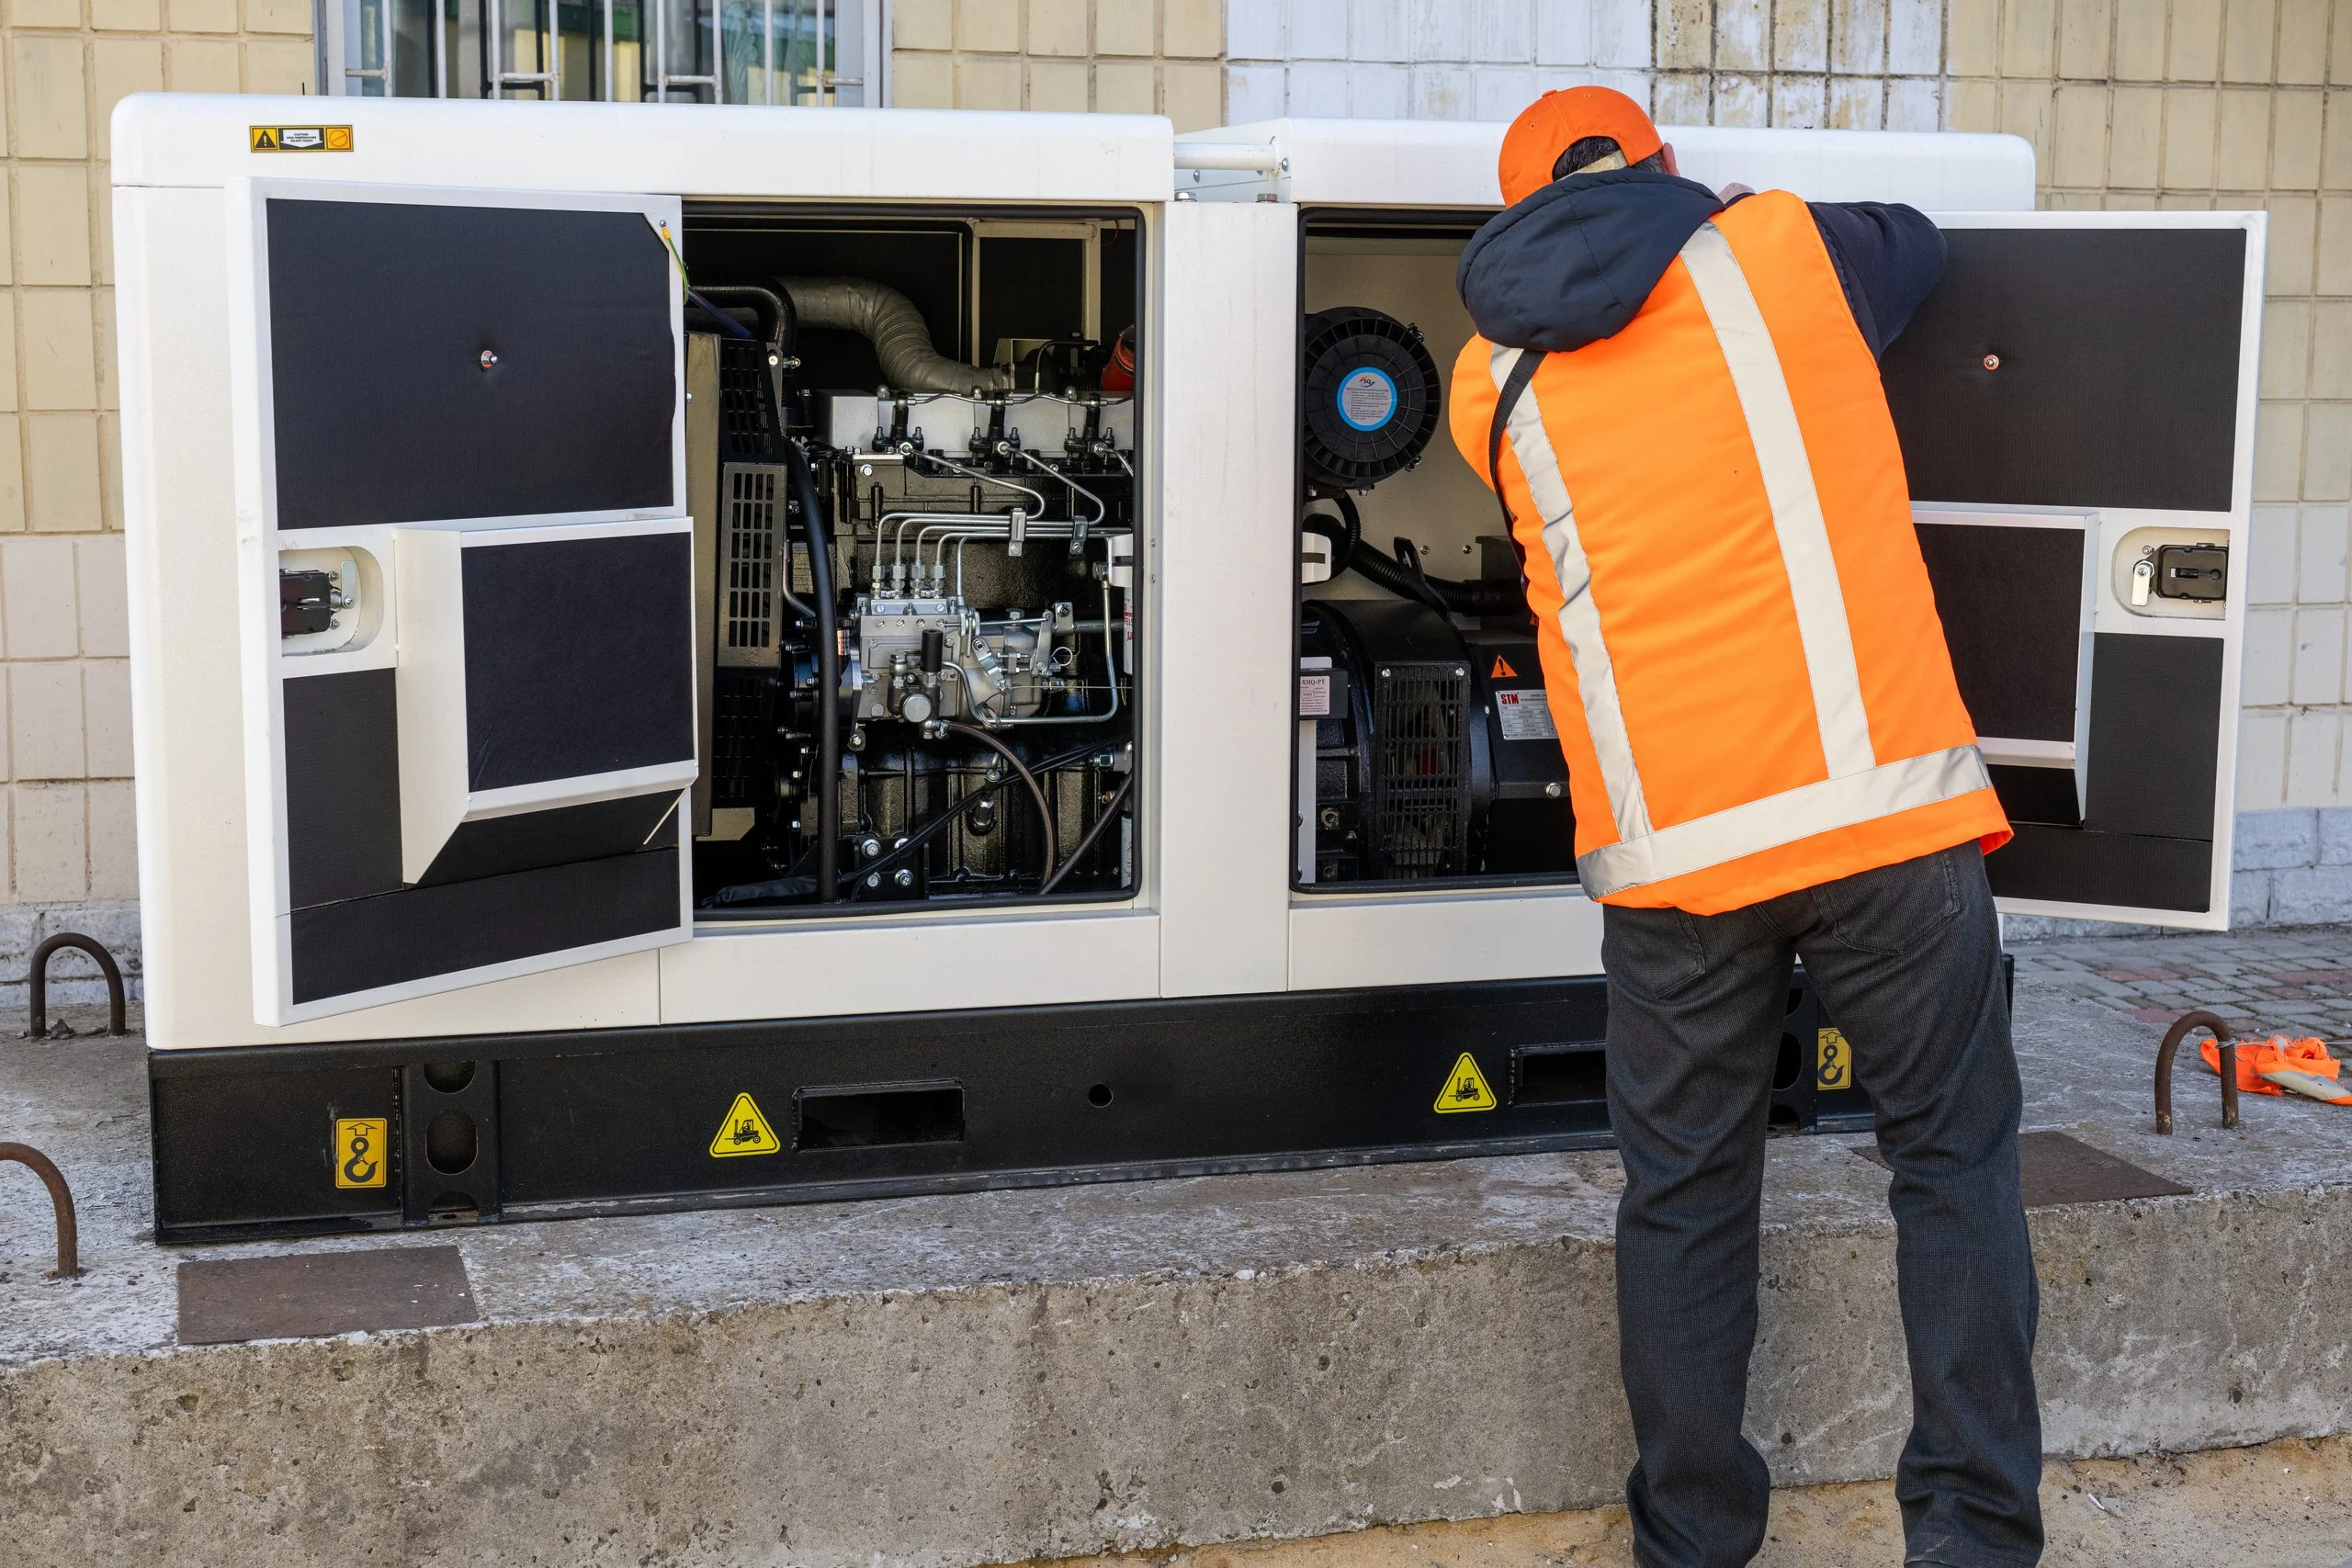
Field technicians routinely work inside cramped, unlit enclosures. Assembly interfaces must be physically mistake-proofed:
- Asymmetric Indexing: design mating faces, connectors, and brackets so they can only be installed in the correct orientation. Offset the locating hole pattern, use a D-shaped bore, or add a tab that prevents 180° misassembly. If a component can be installed wrong, it will be, eventually.
- Staged Locating Pins: use pins with different diameters to prevent partial or rotated engagement. The assembly either fully seats correctly or visibly fails to seat at all.
See more assembly design tips in our Product Assembly Guide.
Accessibility and Service Path Design
Every component with a scheduled service action must be reachable without removing other components first. Design the access path into the machine rather than trusting the service team to figure one out. Keep in mind that specialized service tools can be lost, go missing, or become unavailable at the point of need.
Develop Quantitative Rules for Field Replaceable Units (FRUs)
A Field Replaceable Unit (FRU) is the smallest subassembly or component a technician can remove, renew, and inspect without secondary tear-down of surrounding structural or kinematic assemblies. Every FRU should ideally be designed so its removal doesn’t require special tools, calibration, or other components to be removed first. FRU performance relies on direct geometry constraints that improve accessibility and removability of components.
Design Wear Components for Replacement Efficiency
Intentional design ensures that the task of replacing wear components doesn’t become a bigger job than it should be. The design principle is to isolate the wear element so that the minimum replaceable component is the wear element itself—not the assembly that surrounds it, and never the structure it belongs to.
Sacrificial Wear Liners
Design replaceable, sacrificial liners machined from bearing bronze, wear polymers, or hardened steels. A conveyor guide-rail wear strip that bolts on in five minutes is a consumable. The same geometry machined into the frame becomes a frame replacement or a field-welding operation when it wears through.
Standardization Across the Machine
Where multiple locations can use the same component type, like conveyor guides, seals, and filters, use identical parts.
A machine with twelve different seal sizes creates a twelve-SKU spare-parts inventory, twelve stocking decisions, and twelve chances to have the wrong spare on-site when a line is down. The same machine with two seal sizes creates a two-SKU inventory and a field kit that fits in a technician’s pocket.
Visible Wear Indicators
A technician who can see wear makes a replacement decision before a failure event, converting an unplanned downtime incident into a scheduled maintenance task.
Give wear components visible indicators of remaining service life. These could be a groove that disappears, a colored substrate that becomes visible, or a reference dimension that can be measured with a standard caliper. Sliding components should feature visible, caliper-measurable step-down inspection grooves to ensure technician visibility.
On-Demand Manufacturing and the Maintenance, Repair, and Operations (MRO) Supply Chain
DFS principles are undermined if lead times on critical spare parts span weeks. Maintaining deep component inventories is commercially unsustainable, yet stockouts carry severe plant-level downtime costs.
The Cost of Physical MRO Inventory
Annual inventory-carrying costs for industrial replacement parts can range from 20% to 30% of inventory value. Warehousing costs, tied-up working capital, inventory tracking, and risk of obsolescence from mid-life-cycle machine revisions make deep stocking impractical. Yet conventional batch procurement cycles for custom CNC parts can require weeks of vendor lead time.
A custom housing with a three-week lead time becomes a three-week downtime event if it fails unexpectedly and no spare is on the shelf. A machine with 200 unique custom parts would need spares at every service location for each part whose failure stops the machine.
Design standardization directly reduces inventory carrying costs.
Digital Spare-Parts Architecture via DFM
OEMs can reduce noncritical inventory through a digital MRO model. To make this work, the underlying parts must follow strict Design for Manufacturability (DFM) principles:
- Normalize to Standard Raw Stock: design parts to be machined from standard bar, sheet, or tube stock in common sizes rather than near-net or custom-cut blanks. Standard stock is available on-demand from distributors; custom-cut blanks require a sourcing lead time before machining can begin.
- Optimize Internal Corner Radii: specify corner radii that match standard end mill sizes (R3, R4, R6) rather than sharp corners or non-standard radii. Standard radii clear automated quoting without manual review and machine without special tooling.
- Balance Precision Tolerances: apply tight tolerances only to functional interfaces like bearing seats, alignment features, sealing surfaces. Non-functional surfaces should carry standard tolerances to reduce cost
- Standardize Materials: specify common alloys and tempers (6061-T6, 1018, 304 stainless) rather than specialty grades. Standard materials are stocked by distributors and priced into automated quoting without material sourcing delays.
Parts engineered this way move smoothly through automated quoting environments and into digital manufacturing ecosystems, cutting fulfillment from weeks to days. Design standardization reduces unique parts—and that reduces the number of stocking decisions the service organization has to get right.
Reviewing Replacement Parts Separately
Critical replacement parts should be reviewed for serviceability separately from the original design review. Run every critical subassembly through this technical gate before design freeze:
- Fastener rationalization
- Clearance confirmation
- Hardware retention
- Wear isolation
- Access path verification
- Mechanical extraction
- Poka-yoke verification
- Torque-critical fasteners
- Physical wear indicators
Engineering for Lifetime Margin
When an unscheduled stoppage brings a factory floor to a halt, the end customer does not care about the piece-part savings realized by combining a wear face into a welded frame. Their focus is solely on how quickly the line returns to production and the revenue lost while it sits idle.
Scheduled maintenance and unplanned repairs mean some amount of downtime will always be part of the manufacturing process. Designing for serviceability from the start ensures downtime remains at a minimum.
Streamline Your Replacement Parts Supply with Fictiv
Fictiv helps machine builders and systems integrators manufacture custom spare parts without the burden of physical inventory. Upload your CAD models for instant DFM analysis, design feedback, and fast-turn pricing across precision CNC machining and sheet metal fabrication, from emergency replacements to scheduled production runs.
Upload your part design to get a quote and DFM review.
Talk to a Fictiv expert about your project, or upload your parts to start a free quote.
FAQs About Machine Serviceability and Downtime
How does part design affect machine downtime?
Part design sets how long a repair takes. Fastener types, access paths, alignment features, and wear-part isolation all determine how many steps a technician needs to replace a failed component. A design that adds two hours to the average replacement adds that time to every service event across the installed base, and the cost of that lost production never appears on the part drawing.
What is design for serviceability?
Design for serviceability (DFS) is the practice of designing machine components so technicians can access, replace, align, and reassemble them quickly. It reduces downtime and mean time to repair (MTTR). The design decisions that determine service speed are made early in development, before tooling is cut and the bill of materials is frozen.
What is the difference between design for serviceability and design for maintainability?
The two terms are often used interchangeably in practice. Strictly, maintainability is the broader property of how easily a machine is kept in or restored to working condition. Serviceability focuses on how easily a technician performs service tasks such as access, removal, replacement, and reassembly. Both aim to cut repair time and downtime.
How can machine builders make wear parts faster to replace?
Isolate the wear element so the replaceable component is the wear surface itself, not the assembly or frame around it. Use bolt-on sacrificial liners, standardize identical parts such as seals and guides across the machine, and add visible wear indicators such as caliper-measurable grooves. A technician can then replace parts on a schedule instead of after a failure.
How can on-demand manufacturing support a spare parts program?
On-demand manufacturing lets OEMs hold digital part files instead of deep physical inventory, reducing carrying costs and obsolescence risk. It works best when parts follow DFM principles such as standard raw stock, practical internal corner radii, balanced tolerances, and standardized materials. Those parts move through automated quoting and production more easily, shortening lead times when a replacement is needed.