
Time to read: 12 min
A precision shaft can be machined perfectly, inspected within tolerance, sent for heat treatment, and come back unusable. The shaft may bow, or a bearing journal may lose roundness or move outside tolerance. Reverse the order and a different problem appears. Machining after hardening can increase cycle time, cost, and tool wear or breakage. In both cases, the material and the heat treatment may have been fine. The sequence is what failed. It doesn’t have to be all-or-nothing, though. Many parts are rough machined, heat treated, and then finished.
Heat treatment adjusts material properties, but it can also affect dimensions, residual stress, and surface condition. Material, treatment, sequence, part geometry, machining allowance, and final inspection all have to work as one manufacturing route.
This guide covers common heat treatments for steel and aluminum, when to specify them, and how to plan the manufacturing sequence correctly.
What Heat Treatment Does to Metal and Why It Matters for Machining
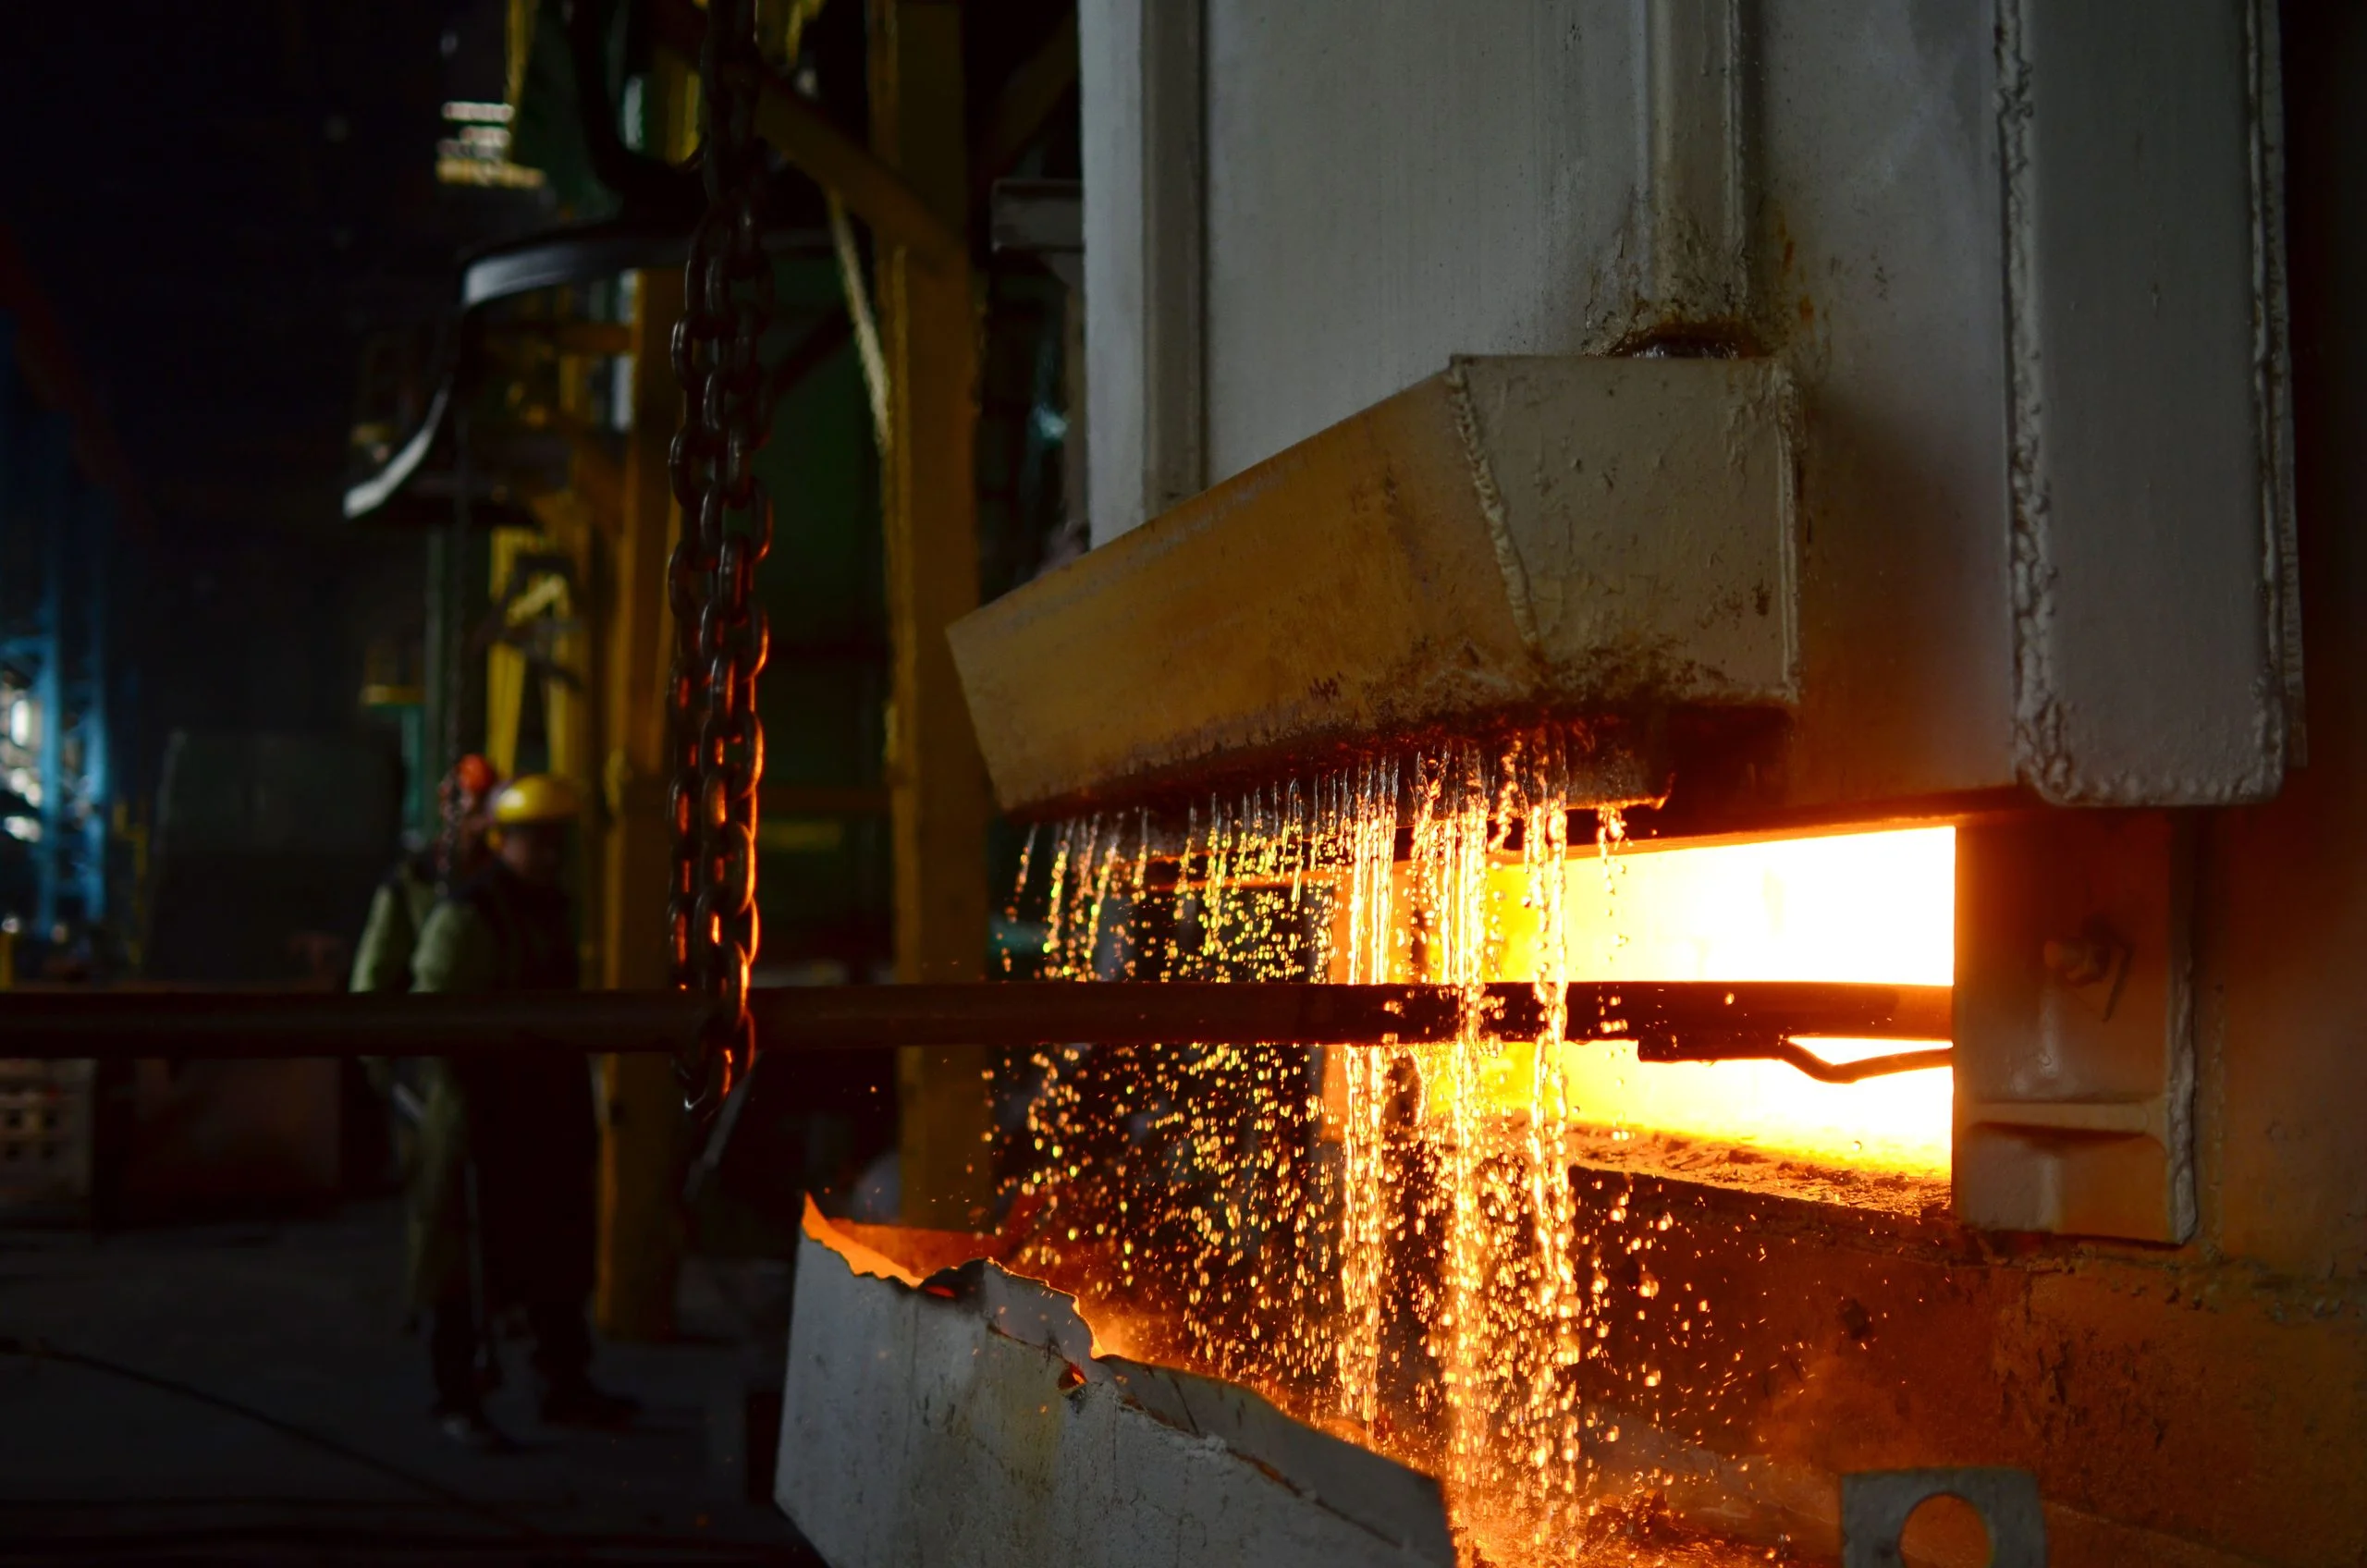
Heat treatment alters a metal’s microstructure to obtain a useful combination of changes in some or all of the material properties: hardness, strength, toughness, ductility, wear resistance, or dimensional stability. The appropriate treatment depends heavily on the alloy and the end-application requirements. Hardenable steels, precipitation-hardening stainless steels, and heat-treatable aluminum alloys reach their final properties by different metallurgical mechanisms.
There are also manufacturing consequences. Heating and cooling can release residual stresses, or create new ones—sometimes both at the same time. Quenching can produce distortion from uneven cooling, and transformations within steel can produce dimensional changes of their own. Thin walls, long shafts, asymmetric parts, and components with large differences in section thickness are particularly sensitive.
For many precision components, the useful starting sequence is rough machine, heat treat, finish machine or grind, and final inspection. This leaves material available to correct distortion and establish critical dimensions after heat treatment. The advisable stock allowance depends on the alloy, geometry, and finishing processes. On hardened steel, that final operation may need to be grinding or EDM, because conventional milling becomes progressively less practical as hardness rises.
Common Heat Treatments for Steel
Steel offers a particularly wide range of opportunities for thermal-process conditioning. Some methods prepare material for machining, while others establish the final mechanical or surface properties.
Annealing
Generally involves heating the steel to an appropriate temperature followed by controlled cooling. Depending on the alloy and annealing cycle, it can reduce hardness, improve machinability, increase ductility, and relieve internal stresses. An annealed condition is useful when the incoming material would otherwise be unnecessarily challenging to machine or form.
Normalizing
Involves heating above the relevant transformation range, followed by open-air cooling. For suitable carbon and low-alloy steels, normalizing can refine the structure and produce a more uniform starting condition, particularly after forging or casting. Normalized steel is normally harder and stronger than the same steel in a fully annealed condition.
The distinction matters in a drawing or purchase specification. “Anneal” and “normalize” describe different processes and shouldn’t be used as generic instructions for making steel softer.
Through Hardening
Typically involves austenitizing, quenching, and tempering. The objective is to obtain the required mechanical properties through the section, subject to the hardenability of the alloy and component size. Tempering after quenching reduces the brittleness of the as-quenched structure and establishes the required balance of hardness, strength, and toughness.
For a machined component, specify the required final condition or hardness where appropriate, for example 40–45 HRC (Rockwell C), together with the applicable material and process specification. Avoid trying to define the heat treater’s furnace cycle, unless the application genuinely requires control of it.
Carburizing (Case Hardening)
Used when the part needs a hard, wear-resistant case (outer surface) with a tougher core. Carbon is introduced by heat into the surface of a suitable low-carbon steel, which is then hardened by subsequent quenching and tempering. A useful specification normally controls both surface hardness and effective case depth, because hardness alone does not define how deeply the hardened layer extends. Effective case depth is typically measured to 50 HRC (or 550 HV). Gears, cams, slides, and other loaded wear surfaces are common applications for carburizing.
Nitriding
This process introduces nitrogen into the surface, producing a hard, wear-resistant layer. Because the process is performed without the severe quench associated with many conventional hardening processes, dimensional disruption is generally reduced. That makes nitriding attractive for precision components or to minimize post-treatment machining, although “low distortion” should never be interpreted as “no dimensional change.” Parts are typically quenched and tempered first, and the case is relatively thin, so nitriding suits wear and fatigue needs more than heavy contact loads.
Stress Relieving
Normally performed below the critical transformation range to reduce residual stresses induced by machining, welding, forming, or prior processing. Importantly, the steel’s pre-treatment hardness and strength remain substantially unchanged. It can be particularly useful before final machining, when a large amount of material has been removed from an initially stable blank.
Heat Treatments for Aluminum Alloys
Aluminum does not harden by forming martensite the way hardenable steels do. Heat-treatable aluminum alloys are strengthened primarily through solution heat treatment, followed by precipitation hardening, or aging.
T6 Temper
The common T6 temper involves solution heat treatment, quenching, and artificial aging. Alloys such as 6061-T6 and 7075-T6 are commonly purchased in this condition already, so a CNC-machined part made from T6 plate or bar does not automatically require another T6 heat-treatment cycle after machining. The alloy itself also matters, as the comparison of aluminum alloys for CNC machining shows.
O Temper
The situation changes if processing alters the material condition. Forming requirements, solution treatment, welding, and subsequent aging may all affect the final temper. Bending 6061-T6, for example, is strongly dependent on material thickness, bend direction, tooling, and bend radius. Tight forming operations are generally better performed in a softer or more formable condition where the production route permits it. It is too broad to state that 6061-T6 simply cannot be formed; large-radius bends are possible, while tighter bends carry substantially increased cracking risk. For this reason, it can be a good idea to specify annealing (O temper) for parts which will be formed or bent before final machining. Parts needing T6 strength after forming must be re-solution-treated and aged, which reintroduces distortion risk.
T73 Temper
For 7075, T73 is an over-aged condition used where improved resistance to stress-corrosion cracking is important. It gives up some of the strength available in T6 in exchange for improved stress-corrosion performance, making the temper decision part of material selection, not merely a heat-treatment note. The T73 temper is commonly chosen over T6 for long-term reliability in aerospace structural applications.
Aluminum also demands careful distortion planning. Solution heat treatment and quenching can move thin, asymmetric, or heavily relieved components considerably. For tight-tolerance work, it may be necessary to establish the required material condition before final machining, then remove the remaining stock from critical bores, faces, and locating features.
Precipitation-Hardening Stainless Steels
15-5 PH and 17-4 PH are in useful territory between conventional stainless steels and high-strength alloy steels. They provide corrosion resistance and substantial strength, and can be machined and then aged to achieve the required final properties. Condition A (solution annealed) is the as-supplied state before aging; parts are typically machined in this condition and then aged.
For 17-4 PH, familiar conditions include H900, H1025, and H1150. The number indicates the nominal aging temperature in degrees Fahrenheit. H900 is associated with high strength, while higher-temperature aging conditions reduce strength and generally improve toughness and stress-corrosion performance. The drawing therefore needs to identify the required condition. Calling out only 17-4 PH leaves an important aspect of the mechanical-property requirement unresolved.
There is also a distinction between a material specification and a heat-treatment specification. A material standard defines the supplied material and product form; a heat-treatment standard controls how a part is subsequently processed. AMS2759/3, for example, specifically establishes heat-treatment requirements for precipitation-hardening corrosion-resistant and maraging steel parts.
The Manufacturing Sequence: When to Machine and When to Heat Treat
Leaving excess material for post–treatment finishing is a principle, not a universal fixed allowance or process route. Consider a shaft with two bearing journals and a spline. The blank may be turned with stock left on the journals, then hardened and tempered. The journals can subsequently be ground to final diameter, roundness, and surface finish. Features that do not require comparable precision may already be near finished size before treatment.
A nominal rough-machining allowance such as 0.5 to 1.0 mm may be reasonable on some parts, but it should not be applied indiscriminately. A small precision component, a long slender shaft, and a large forging can require very different allowances. Previous heat treatment, section changes, quench method, and residual stress from machining all affect the result.
If a hardened feature cannot reasonably be machined conventionally, EDM can provide another finishing route, although the recast and heat-affected surface produced by EDM must itself be considered where fatigue or surface integrity is critical.
Surface finishing can add another process constraint. High-strength steels exposed to plating, pickling, stripping, chemical milling, etching, and related processes may absorb hydrogen. AMS2759/9 covers hydrogen-embrittlement-relief baking of heat-treated steel parts following processes capable of introducing hydrogen. The applicable finishing and material specifications should establish the required bake temperature, duration, and permitted delay before baking. Those parameters should not be copied from another drawing simply because the alloy or plating appears similar.
Common Component Treatments and Sequence
| Component | Typical material | Common treatment | Sequence note |
| Gears | 8620, 4140 | 8620 – Carburize, harden, temper 4140 – Nitride or induction harden | Leave stock; finish-grind or hone as required |
| Shafts | 4140, 4340, 1045 | Through harden and temper, or induction harden | Rough machine, treat, grind journals |
| Bearing races/rings | 52100 | Through harden, temper | Grind after treatment |
| Cams and followers | 8620, tool steel | Carburize or through harden | Finish-grind lobes after treatment |
| Fasteners and pins | 4140, 17-4 PH | Harden and temper, or age | Check hydrogen relief if plated |
| Aerospace brackets | 7075, 17-4 PH | T73/T7351; H900–H1150 | 17-4 PH – Machine in Condition A (solution annealed), then age7075 – Machine from stock |
| Tooling and dies | A2, D2, H13 | Vacuum harden, temper | Rough, treat, finish by grinding or EDM |
How to Specify Heat Treatment on an Engineering Drawing
A useful heat-treatment callout tells the manufacturer what final condition the part must meet, and identifies the governing specification where required. The drawing’s dimensional and geometric requirements still need to define the finished part clearly.
Through Hardening
For a through-hardened steel part, a note might state:
HEAT TREAT TO 40–45 HRC PER APPLICABLE PROCESS SPECIFICATION.
Carburizing
A carburized gear requires more information:
CARBURIZE AND HARDEN. EFFECTIVE CASE DEPTH 0.75–1.25 mm TO 50 HRC. SURFACE HARDNESS 58–62 HRC.
Those numbers are illustrative only. Case depth must be selected based on the gear geometry, contact stress, tooth size, loading, and applicable design requirements, rather than copied from a generic example.
Post-Grinding
Where final grinding is required, say so:
GRIND BEARING JOURNALS TO DIMENSIONS SHOWN AFTER HEAT TREATMENT.
This small note removes an important ambiguity. The drawing now establishes that the journal dimensions apply to the finished hardened component, not to the part entering the furnace.
The same principle applies to aluminum and precipitation-hardening stainless steel. State the alloy, required temper or aging condition, applicable heat-treatment specification, and any additional machining or inspection requirements.
Fictiv’s manufacturing network can combine CNC machining and secondary operations within the same sourcing program, allowing heat treatment, finishing, and final dimensional requirements to be considered as connected manufacturing steps.
Upload your CAD today for a quote that includes heat treatment or post-processing.
Talk to a Fictiv expert about your project, or upload your parts to start a free quote.
FAQs About Heat Treatment for Steel and Aluminum
Should I heat treat before or after machining?
For most precision parts, rough machine first, heat treat, then finish machine or grind. Heat treatment can cause distortion and dimensional change, and leaving stock lets you correct it and hold critical tolerances on the finished part. The right allowance depends on alloy, geometry, and process, so confirm it with your manufacturer. Hardened steel usually needs grinding or EDM for the final pass, because conventional milling gets less practical as hardness rises.
Does CNC-machined aluminum need heat treatment after machining?
Usually not. Alloys such as 6061 and 7075 are commonly supplied in a heat-treated temper like T6, so machining from that stock doesn’t require another cycle. Solution heat treating a finished part invites distortion. Forming, welding, or a specific temper requirement, such as T73 for 7075, can change this, so state the required temper on the drawing.
What is the difference between annealing and normalizing steel?
Annealing heats steel and cools it in a controlled, slow manner to soften it, improve machinability and ductility, and relieve internal stress. Normalizing heats it above the transformation range and cools it in air, which refines the structure and produces a more uniform material that is normally harder and stronger than annealed steel. They aren’t interchangeable, so call out the specific process on your drawing.
Which heat treatment causes the least distortion?
Nitriding generally causes less distortion than quench-hardening processes because it runs without a severe quench. It isn’t distortion-free, though. Stress relieving before final machining also reduces movement from machining-induced stress. Thin walls, long shafts, and asymmetric parts are the most sensitive, whatever the process.
How do I call out heat treatment on an engineering drawing?
Specify the final condition the part must meet, not the furnace cycle: alloy, hardness or temper, and the governing specification. Carburized parts also need effective case depth and surface hardness. For 17-4 PH, state the condition, such as H900 or H1025. If finishing follows heat treatment, add a note such as “Grind bearing journals to dimensions shown after heat treatment.”